CAPABILITIES
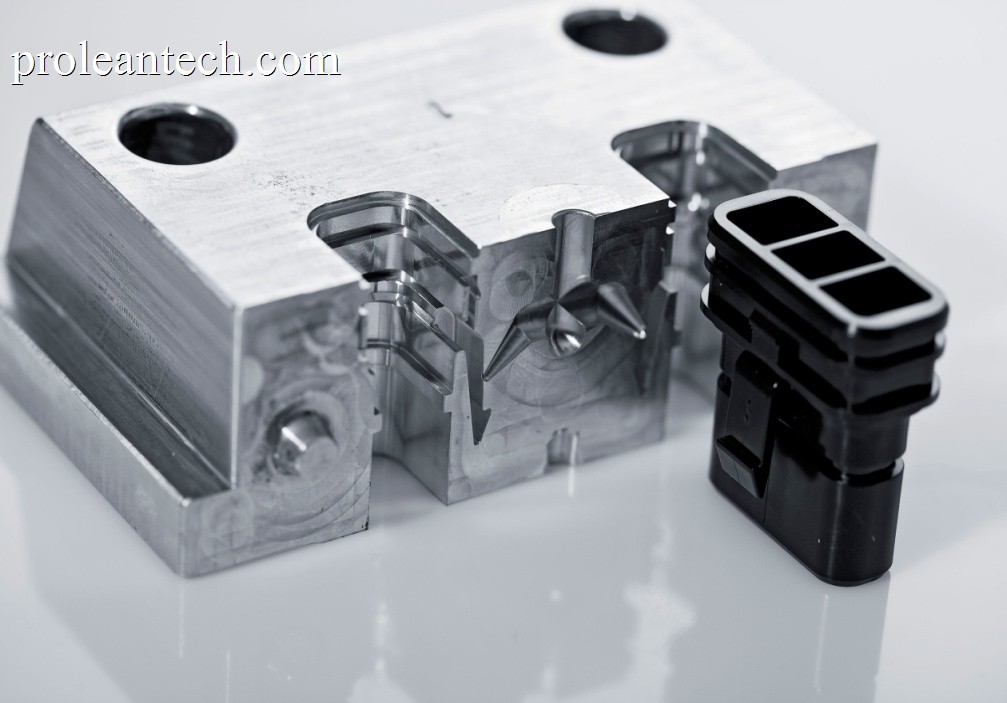
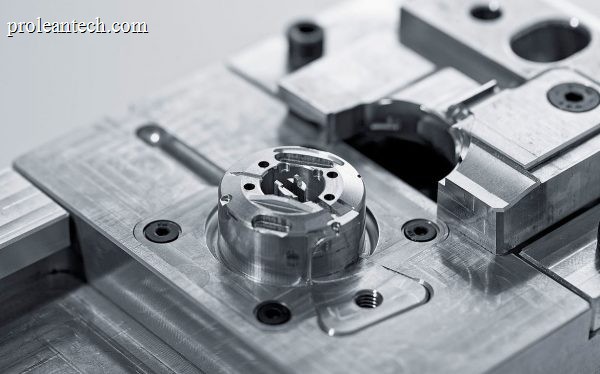
Rapid tooling, also known as rapid injection mold tooling, is a quick and economical injection molding solution for small batches of parts. Industries depend on rapid tooling for small batches during the testing and prototyping stages.
Prolean offers quality rapid tooling injection molding services for a broad range of materials in convenient quantities.
All uploads are secure and confidential.
Precision Parts. Endless Possibilities.
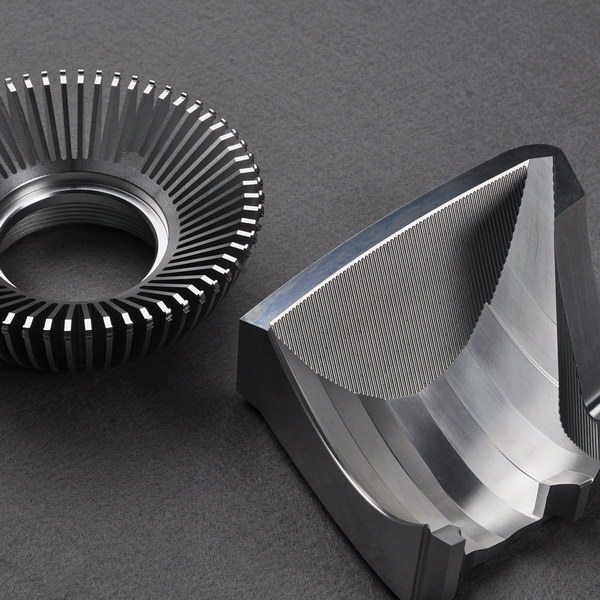
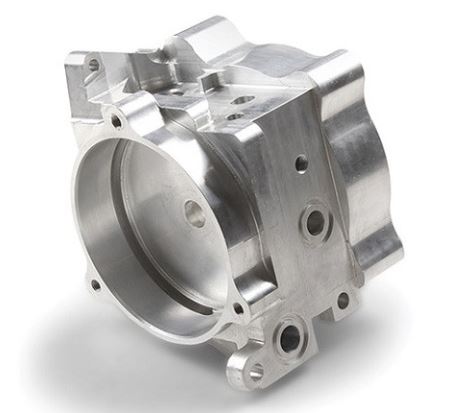
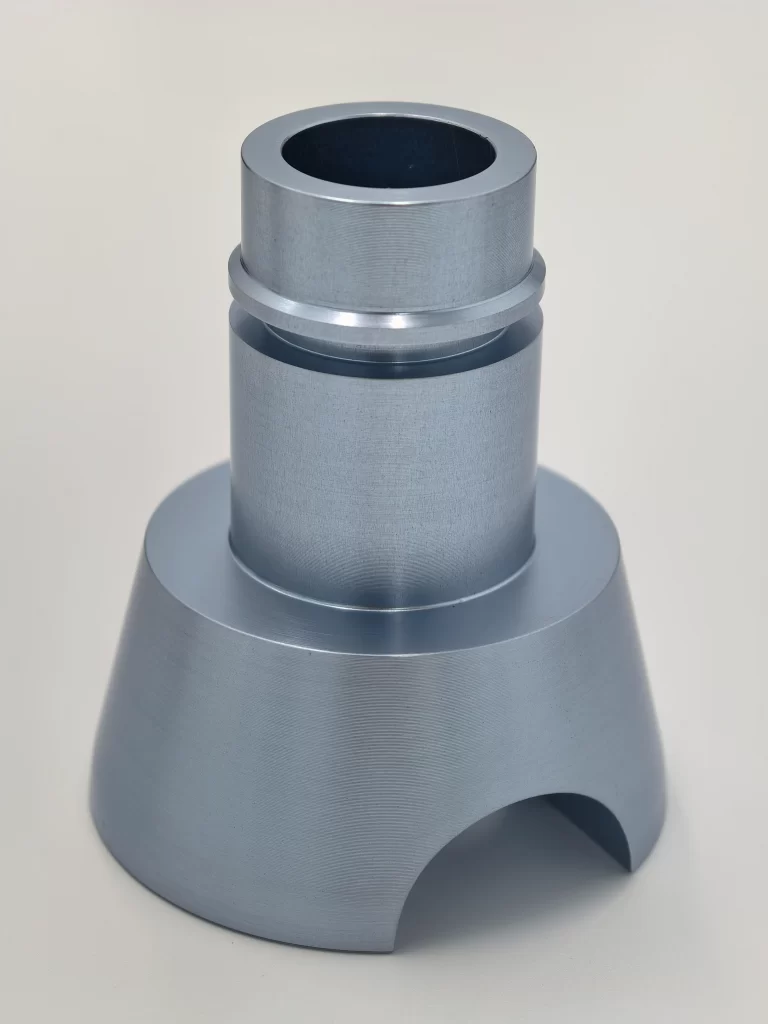
Explore our custom manufacturing capabilities through real product examples.
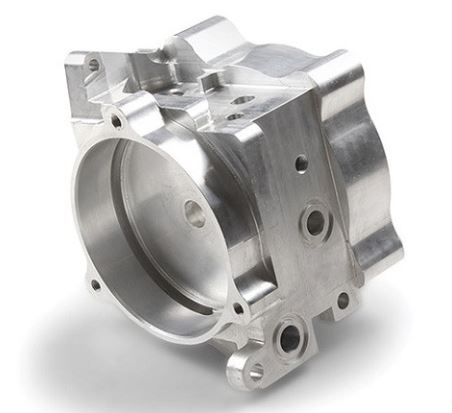
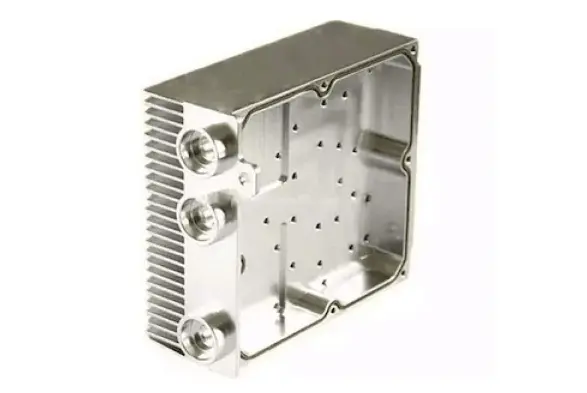
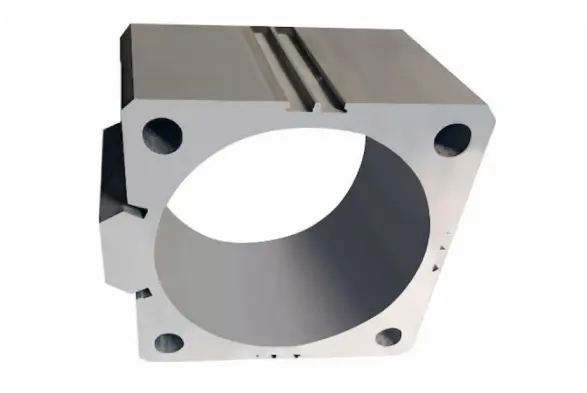
Prolean’s Rapid Tooling Service
Rapid tooling is also known as bridge tooling or prototype tooling because it is a cost-efficient production process for parts that are not ready for mass production but require more quantities than the primary prototyping stage.
Rapid tooling utilizes steel or aluminum molds for injection molding of plastic parts. The steel and aluminum molds are perfect for batches as large as 10,000 and take just one or two weeks with existing CAD tools to design. The produced parts are as good as or almost close to mass-production parts in quality.
Advantages of Rapid Tooling
Rapid tooling is ideal for products not yet ready for mass production. The quick production allows companies to test a larger batch of product in its near-mass production state without investing time and resources in production tooling. The prototypes and test batches are great at revealing flaws in the design of the product. Imperfections like weak spots, warping and shrinking found by rapid tooling can save significant amounts of capital for companies.
Rapid tooling is also cheaper than other prototyping processes for larger batches which makes it perfect for young companies looking to get a small batch out in the market.
How to Order Parts?
Get a free quote from a real engineer; once we receive your design, our engineer will review it and send you a quote as fast as one hour.
Get an Instant Quote
Upload your design file or email our engineering team directly. You'll get a firm quote in as fast as one hour, no account required.
Start Production
Once you confirm your order, production begins immediately. Track real-time status from cutting through final inspection via your order dashboard.
Receive Your Part
Every part passes quality control before it ships. We pack parts to prevent damage in transit and deliver directly to your address.
We generally evaluate production and provide quotations within one hour. If you need a more urgent quote immediately, please contact us through our official WhatsApp account.
Rapid Tooling Materials Options
| Thermoplastics | |
| ABS | PEEK |
| PC | PET |
| Nylon (PA) | PMMA |
| Glass Filled Nylon (PA GF) | POM |
| PC/ABS | PP |
| PE/HDPE/LDPE | PVC |
| TPU | |
Rapid Tooling Material Guide
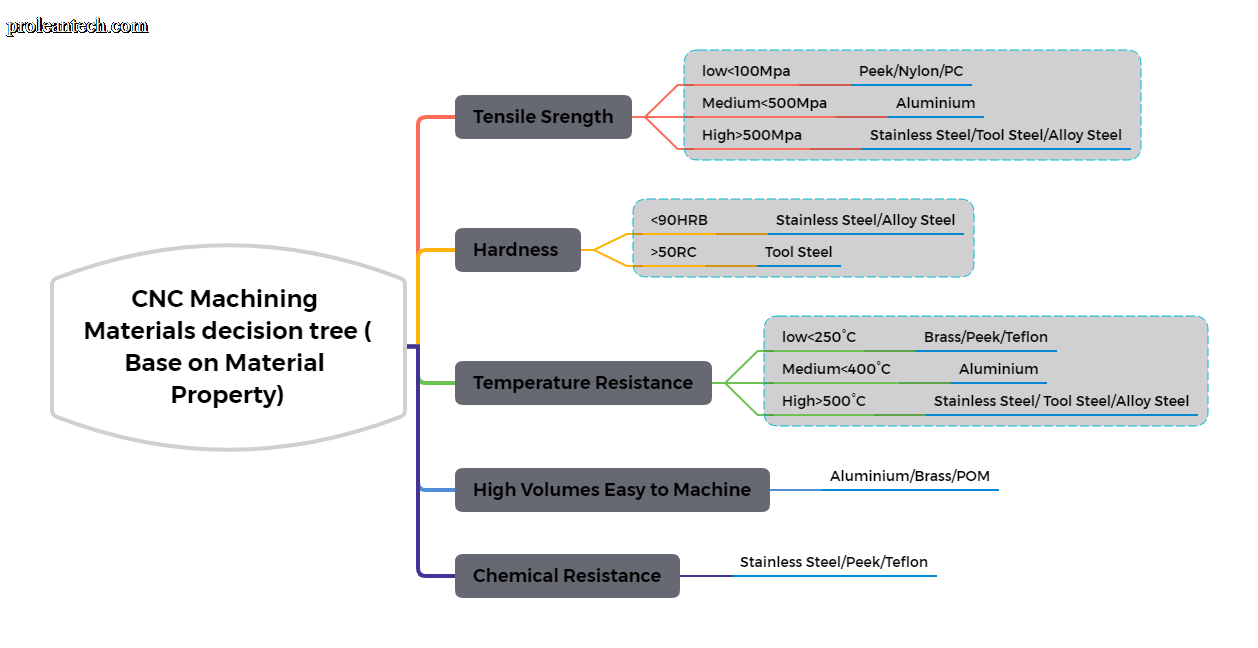
Finishing Options For Rapid Tooling Service
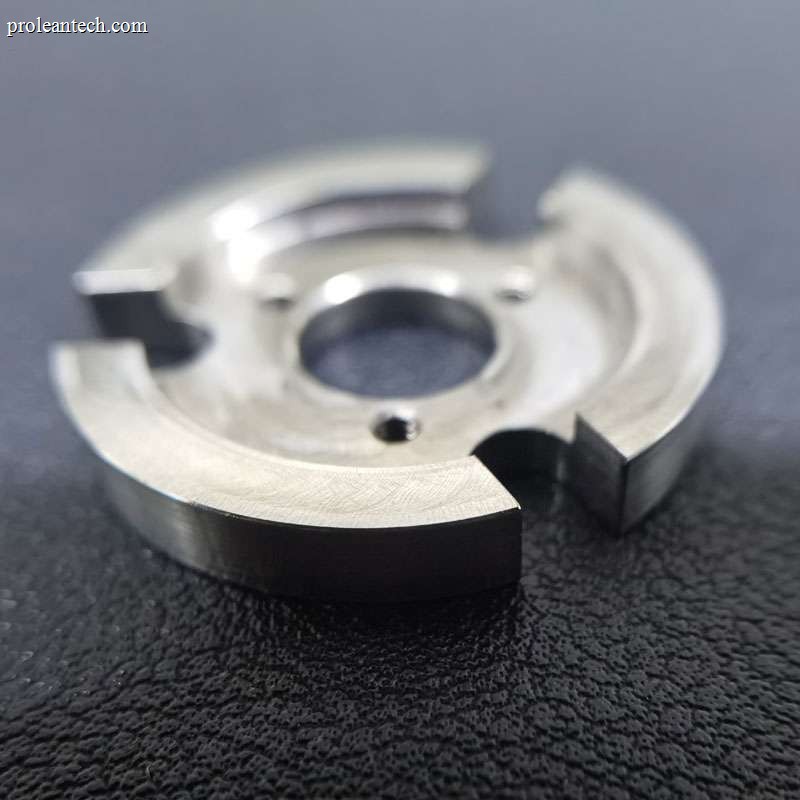
As the machined or deburring
The machined or deburring finish is the standard finish where unwanted attach chips are removed with deburring tools, and sharp edges are chamfered to smooth the surface (3.2 μm).
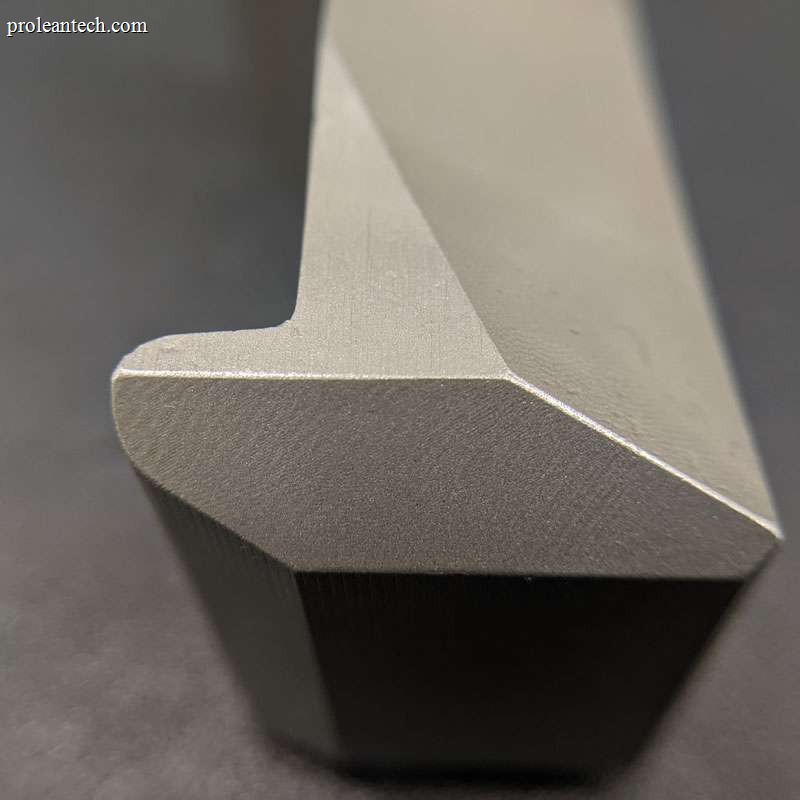
Bead Blasted
Bead blasting produces a matte texture, removing all the marks of machining tools. It applies to ABS, Aluminum, Brass, Stainless Steel, and Steel parts.
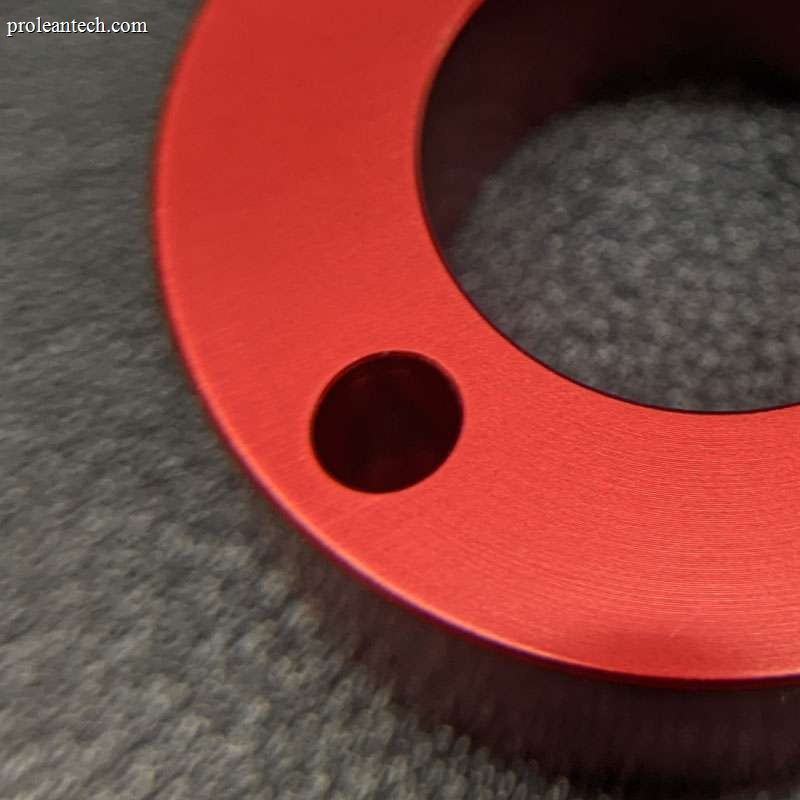
Anodizing
Anodizing involves adding an aluminum oxide coating to aluminum and its alloys. The layers, which come in various colors, increase strength and shield the surface from corrosion.
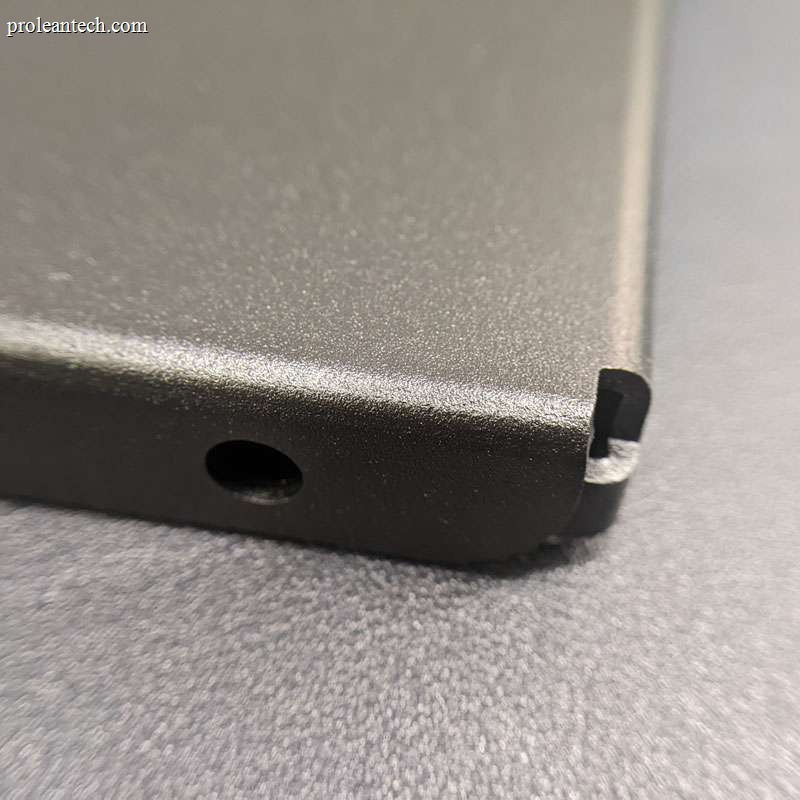
Powder coating
Powder coating is the electrostatically applying of dry powder to the surface. It produces a thin layer providing excellent resistance to wear, corrosion, and abrasion.
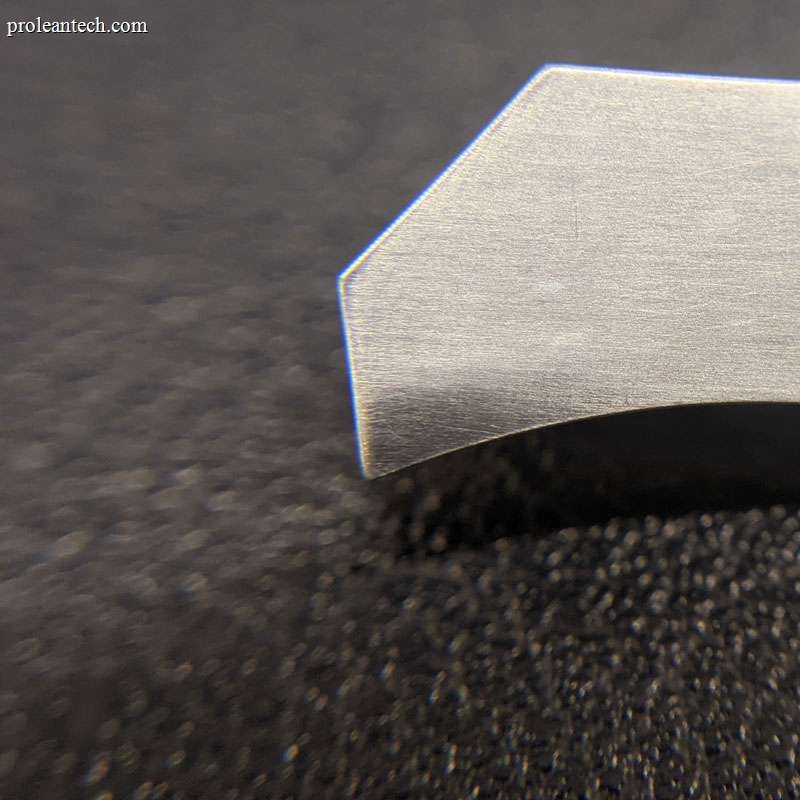
Polishing
Physical rubbing of a metal surface to create a shiny surface is called a polishing surface finish. It increases the reflectivity and does not affect the dimensional stability of parts.
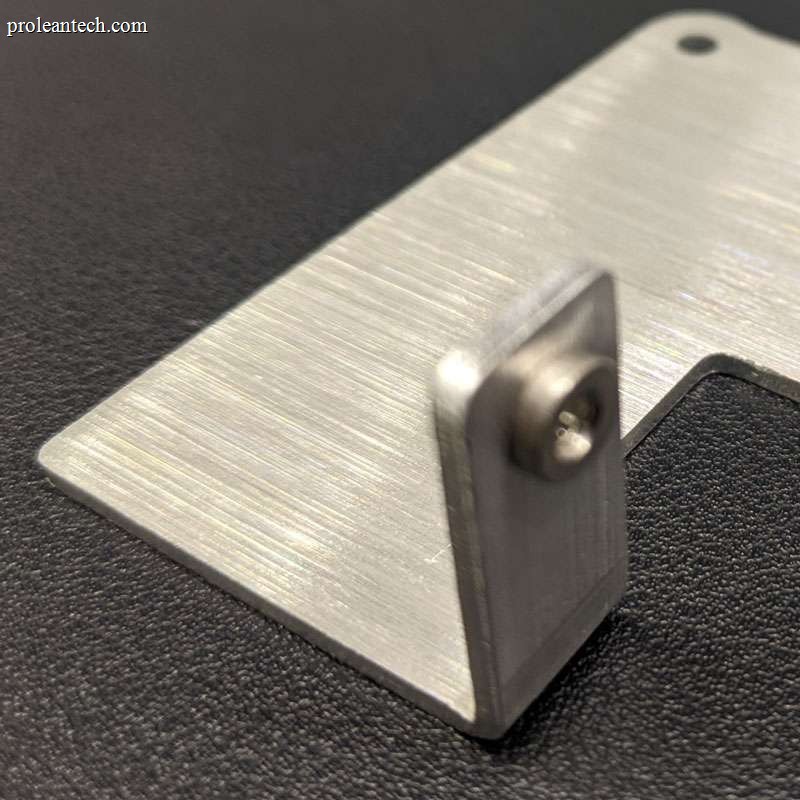
Brushing
Brushing is achieved by applying an abrasive brush to the metal surface, which produces a unidirectional satin finish. And it is not recommended for highly corrosive materials.
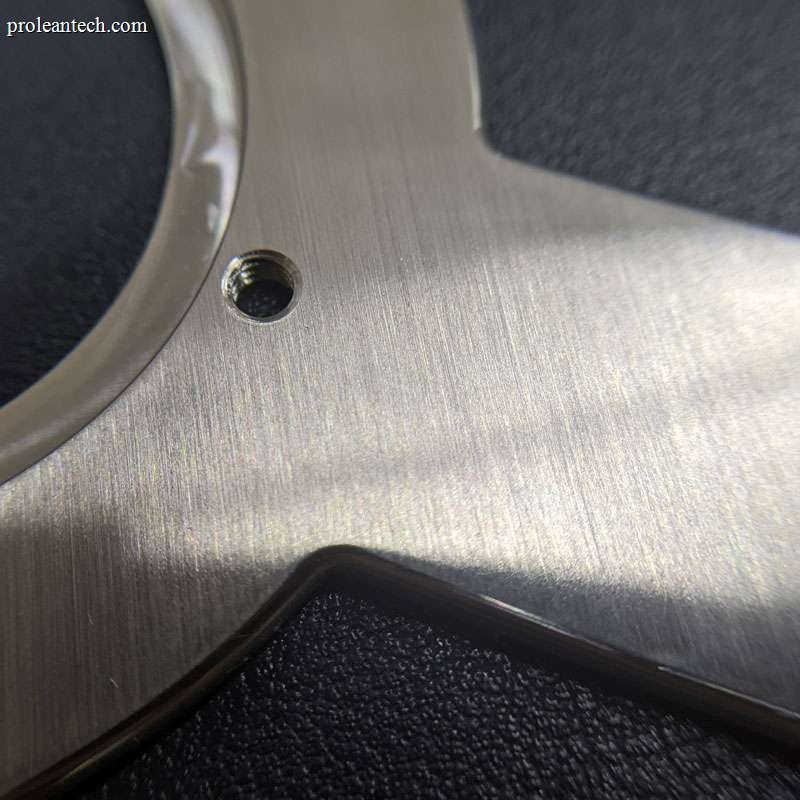
Smooth machining
Smooth machining is done by controlling the machining process, such as feed rate & cutting speed. It minimizes the tool marks and risk of corrosion.
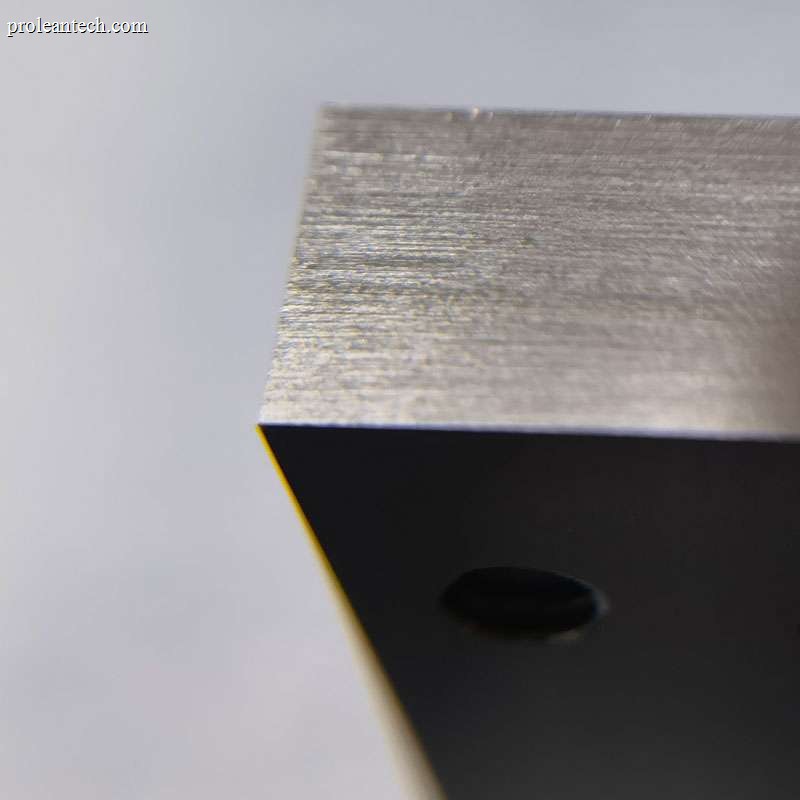
Black-Oxide
Black oxide finish reduces surface reflectivity and offers mild corrosion protection. It involves adding a thin layer of magnetite to the surface.
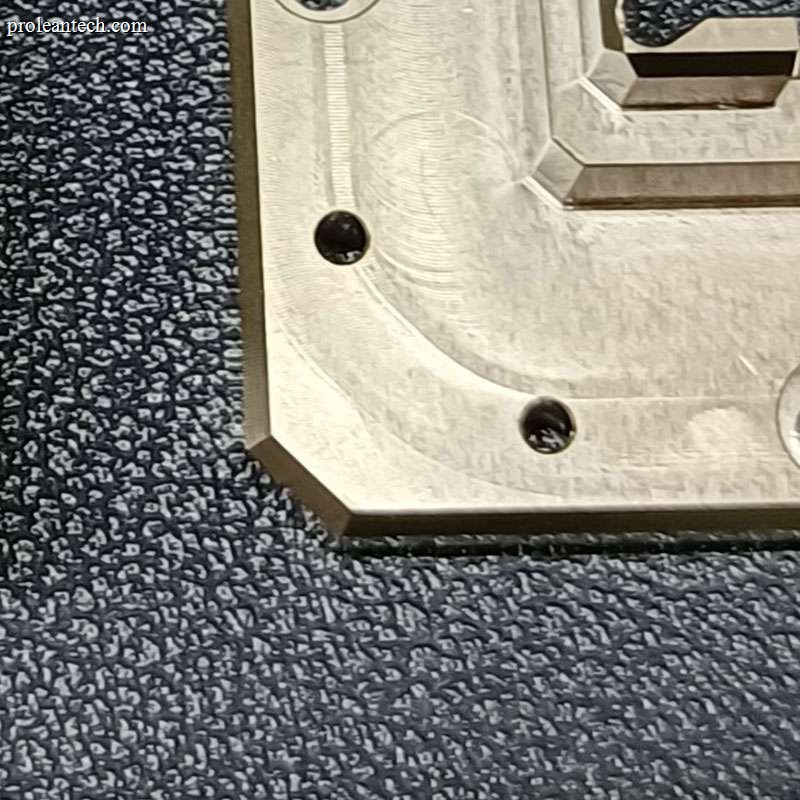
Electro-less Nickel Plating
A thin layer of Nickel is created on the surface from a nickel-containing solution without electrolysis. Electro-less nickel plating provides a shiny appearance, excellent hardness, abrasive, wear, and corrosion-resistance to the substrate material.
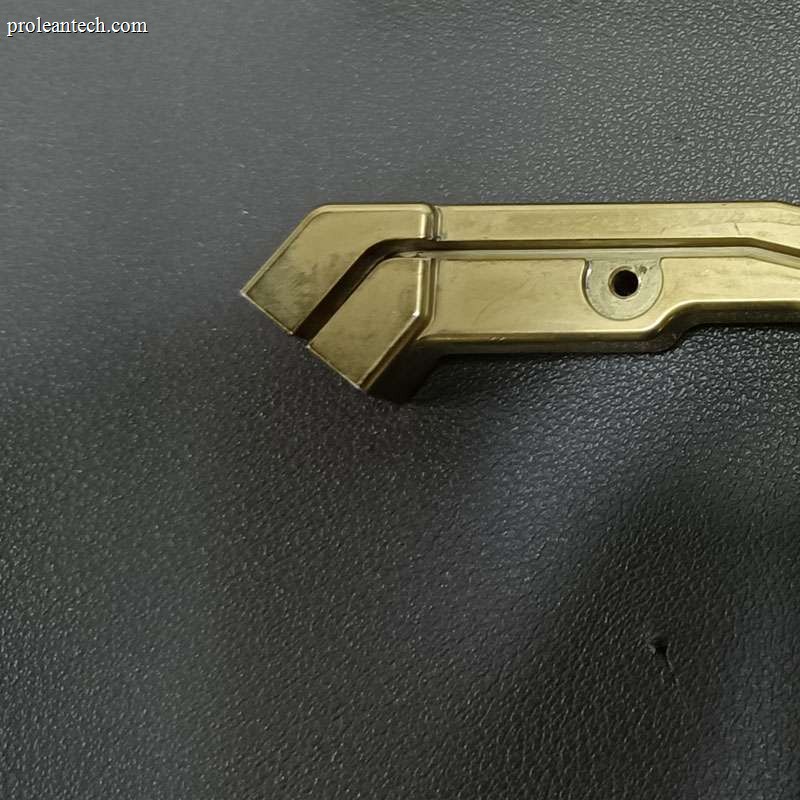
Alodine
Provides excellent corrosion resistance property to the aluminum parts with greenish-gold color. It is the low-cost and quick surface finishing approach.
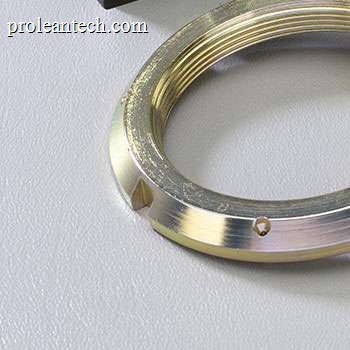
Electroplating
Electroplating increases the hardness of the steel &aluminum parts. It offers excellent corrosion, wears, and abrasion resistance.
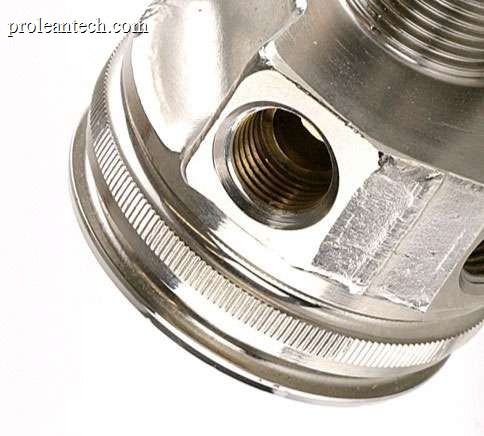
Nickel plating
Make the parts super resistive to corrosion. It enhances mechanical strength, hardness, wear resistance, lubricity, and ductility. Nickel plating is applicable in different materials, including Steel, aluminum, copper, and brass.
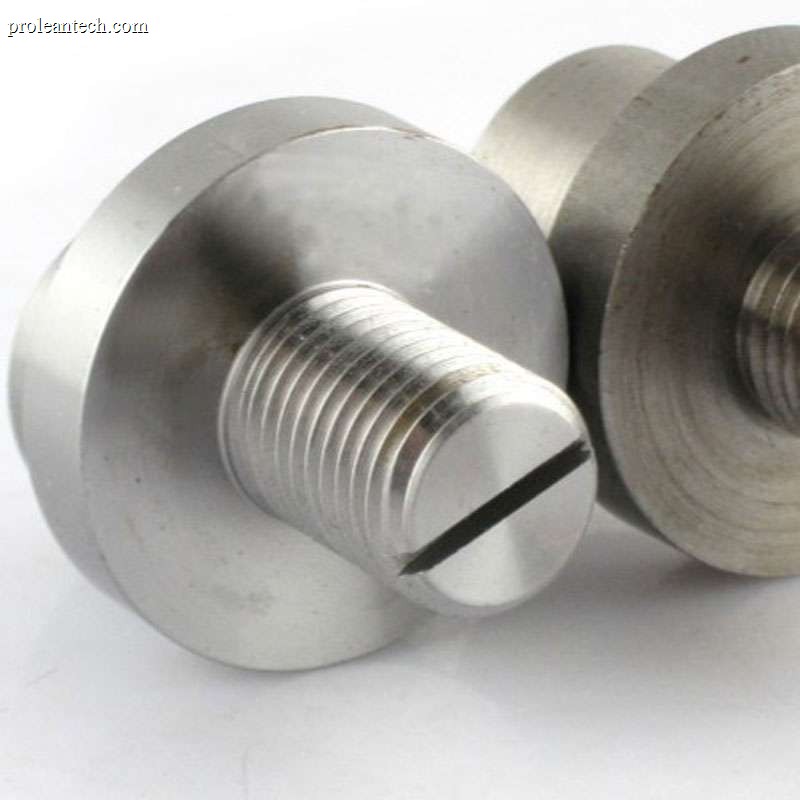
Passivation
Enhance the appearance and functionality of the parts. After Passivation, parts of Steel and its alloys become super resistive from corrosion.
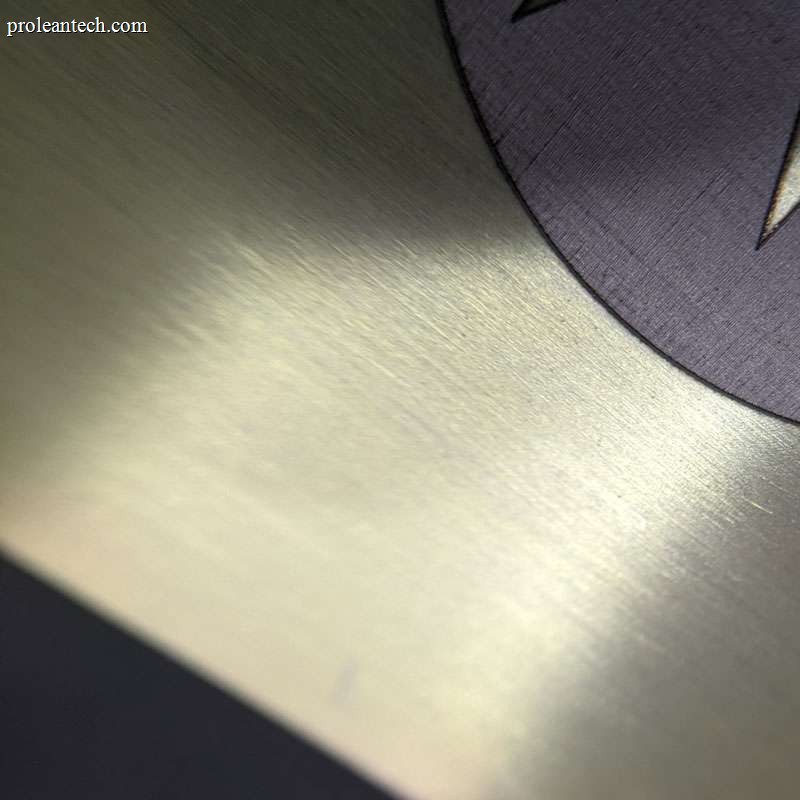
Yellow Chromate conversion coating
A shiny appearance with goldish color provides excellent corrosion resistance. It is applied on the surface of aluminum, magnesium, and their alloys. A layer of chromate also enhances the conductivity of parts
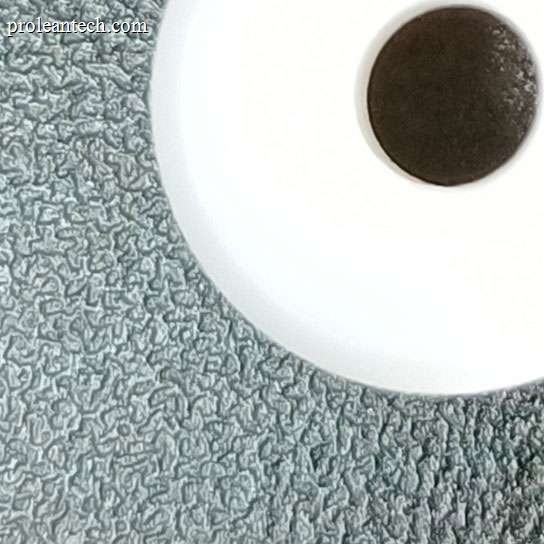
PTFE (Teflon) Coating
The Teflon layer on the parts offers excellent corrosion resistance, water resistance, and non-stickiness with a non-reactive surface.
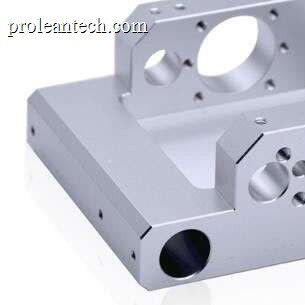
Fine machining
The higher-precision machines produce delicate machining surfaces by utilizing sharper tools and regulating feed rate and cutting speed. Surface roughness up to Ra 0.8 μm can be maintained with smooth machining.
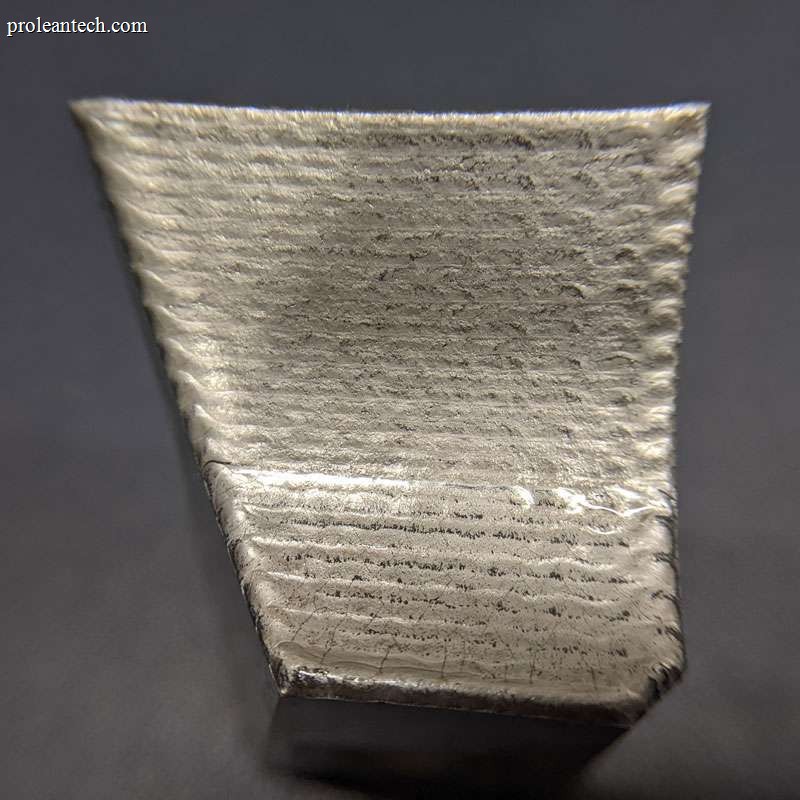
Laser Cladding
Provides excellent corrosion, wear, and abrasion resistance. Laser Cladding is also effective for treating minor surface imperfections such as cavities, tiny cracks, and rust damage.
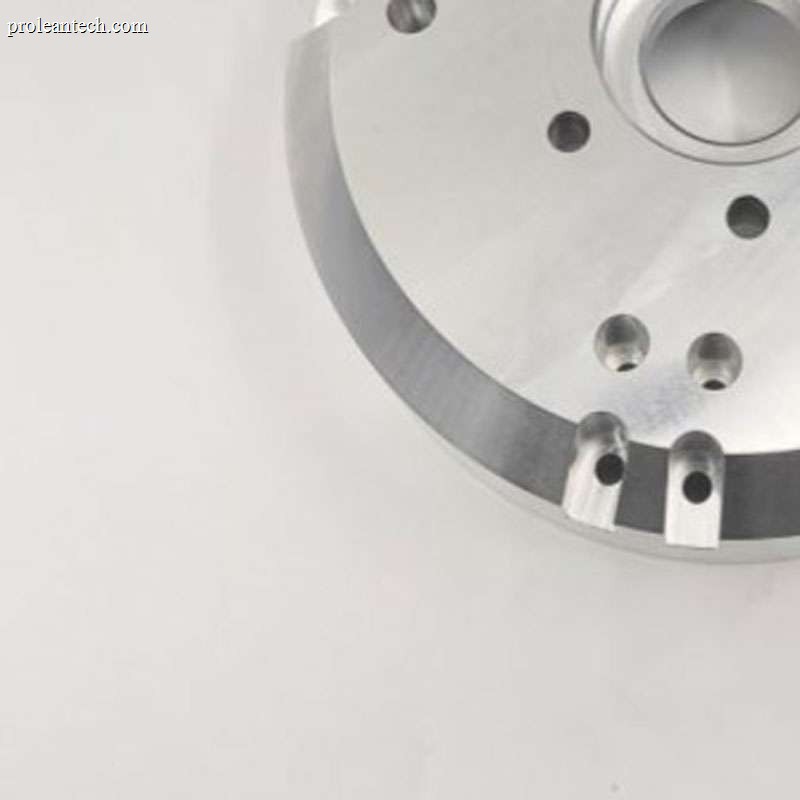
Sanding
Provides a random, non-linear texture with a shiny, high gloss finish. However, it might be unable to create sharp corners and pockets
More
Provides a random, non-linear texture with a shiny, high gloss finish. However, it might be unable to create sharp corners and pockets
3 Ways to Ensure Perfection
Standards
GENERAL TOLERANCE
For metals, the standard is ISO-2768 fH (fine)
For plastics, the standard is ISO-2768 mK (medium)
Metric threads tolerances:ISO 965-1 standard UN Threads Tolerances: ASME B1.1-2003 standard
knurling: ISO13444:2012 standard Our factory is ISO 9001:2015 certificated
Visual inspection and Protection
Constant visual inspection conditions
Quantification of cosmetic surface quality
Process requirements
Part cleaning and Protection
Quality Inspection Report
Inspection Confirmation
Dimensional confirmation
Appearance confirmation
Quality documentation
See why customers dig us
It has been a true pleasure working with ProleanTech for our Plastic Injection Molding needs. I appreciate your patience and the time you've dedicated to finalizing all the details.
-Steven Edwards, Lead Die Casting Engineer
We contacted ProleanTech for aluminum injection molds back in 2022. I can not believe, they deliver the first batch within a week.
-Jessica Scott, Product Development Manager at InnovateMetal Works
We are extremely pleased with your production tooling service, whether it was the first order of custom fixtures or a recent casting mold. And we will continuously work together in the future.
-Christopher Hill, PrecisionProto Labs
Your attention to detail and quality in plastic injection mold manufacturing is commendable. The services are reliable, and we are highly satisfied with the final results.
-Maria Turner, MolderWorks Manufacturing
As an US company I first hesitate to outsource from china due to misunderstanding about tarrifs. Later, i found why comapnies are partnering companies like proleanTech. Thank you!
-Andrew White, Surface Treatment Specialist at CoatPro Solutions
We're impressed with ProleanTech's exceptional service and quality in plastic injection molding. They delivered excellent results, which made them our trusted partner.
-Nicole Rogers, Director of Manufacturing at CustomMold Solutions
Related Blog
Common Injection Molding Applications, Design Features, & Tips
Injection molding applications range from aircraft components and automotive parts to medical devices, electronic housings, construction fittings, and agricultural components.
TPE Injection Molding: Types, Process, and Design Guidelines
TPE injection molding is widely used for seals, grips, and medical components.
PVC Injection Molding: Pros, Cons, Design & Applications
PVC injection molding is used to make pipes, fittings, electrical housings, valves, and connectors.
Latest Blog
Check out our latest blogs, we share industry trends, design tips, and experience earned from manufacturing.
- Electroplating Vs Electro-less plating
- What are the types of surface finishes for CNC machining?
- Common Materials for CNC Machining
- Tolerances in CNC Machining
- Sheet Metal Fabrication: Enclosures for Electronics
- Best Cutting Tools for CNC Machining– Choose the Right
- An Ultimate Guide to CNC Copper Machining
- Production Cycle Time in CNC Machining
Die Cast Industry: Status in 2026 and Trends by Segments
Die-casting is a process of creating metal components by forcing molten material into a reusable mold (called a die), where it fills the cavity and takes the shape upon solidification.
Read more →
Electric Discharge Machining Applications Across Industries
Electrical Discharge Machining (EDM) is a non-conventional subtractive manufacturing process, in which a tool (electrode/wire) removes the material from conductive workpieces using controlled electric sparks inside a dielectric medium
Read more →
PEI CNC Machining: Material Grades, Processes, and Considerations
PEI CNC machining converts raw PEI rod, bar, or plate into functional components using cutting, milling, turning, drilling, and other suitable operations using the CAD model & CNC program.
Read more →BRIDGE-TOOLING REVIEW
Define what the short-run tool must prove before scale-up
Rapid tooling sits between a prototype and production asset. Its value comes from confirming part geometry, material flow, shrink response, cosmetic limits and secondary operations before committing the full production tool.
Engineering data to lock before release
| Part priority | Functional surfaces and high-risk geometry |
|---|---|
| Material route | Prototype resin versus production-intent resin |
| Tooling life | Expected quantity and allowable wear |
| Scale-up evidence | Dimensional trend, cosmetic review and change log |
Short-run tooling should have explicit life and material assumptions; neither should be inferred from a prototype drawing alone.